


Sections
- Wastewater production in the pharmaceutical industry
- Effluent management in drug production
- Treatment of biodegradable discharge
- Vacuum evaporation for difficult-to-treat effluents
- Advanced oxidation processes (AOP)
- The need for a personalized and integrated solution for each case
Wastewater production in the pharmaceutical industry
The pharmaceutical industry uses large amounts of purified water for the manufacture of medicines and other healthcare products. It also consumes water in cleaning and sanitation operations of equipment, reactors, tanks, pipelines, and primary packaging.
As a result of these processes, effluents are generated containing residues of chemicals, traces of active pharmaceutical ingredients (API), solvents, detergents, and other compounds used during production.
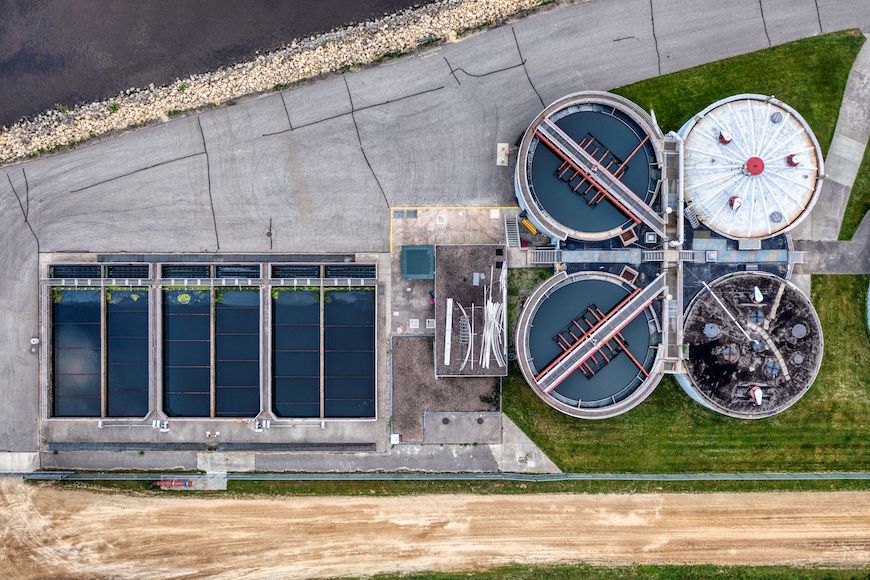
The World Health Organization (WHO) points out that a wide variety of waste generated by the pharmaceutical sector ends up reaching the environment through effluents from manufacturing facilities.
The volume and composition of these wastewaters show high variability, as they depend on the type of medicine produced, the raw materials used, production processes, cleaning protocols, and the different technologies employed at each plant.
Numerous chemical substances, cleaning products, and so-called active pharmaceutical ingredients (API), responsible for the therapeutic effect of medicines intended for prevention, treatment, or diagnosis of diseases, are involved in pharmaceutical manufacturing.
Effluent management in drug production
Wastewater generated by the pharmaceutical industry presents high variability in both flow and composition, making its treatment a significant technical challenge.
During drug manufacturing, streams with very different characteristics may be generated: wash waters with biodegradable organic matter, effluents with active pharmaceutical ingredients (API), solvents, cleaning and disinfection products, refractory compounds, as well as streams with very high salt concentrations.
This heterogeneity makes it especially important to apply a strategy of effluent segregation at the source, avoiding indiscriminate mixing of streams with very different characteristics before treatment.
Why shouldn’t all effluents be sent to biological treatment?
The operation of a biological reactor depends on maintaining an active population of microorganisms and suitable environmental conditions for their metabolism.
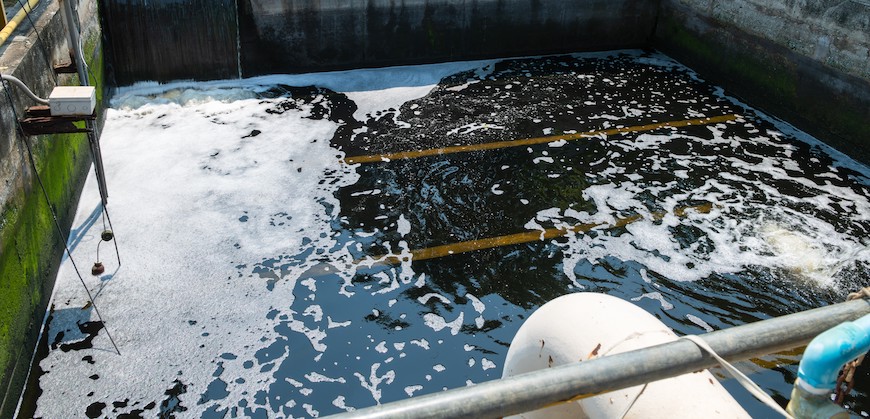
The entry of certain streams from the production process can alter these conditions and significantly reduce treatment performance. Among the most problematic are:
- Effluents with active pharmaceutical ingredients (API), such as antibiotics, disinfectants, or other biologically active compounds, which may exert toxic or inhibitory effects on microorganisms.
- Streams with high concentrations of solvents or other organic compounds, which can cause COD spikes and, depending on their nature and concentration, inhibit biological activity.
- Effluents with high salinity, which can cause osmotic stress on biomass and reduce its metabolic activity when concentrations exceed levels tolerated by the process.
- Streams with a high proportion of refractory or non-biodegradable organic matter, whose incorporation into the reactor increases the COD load without microorganisms being able to effectively remove it.
- Concentrated and variable composition effluents, which can generate peak loads that destabilize reactor operating conditions.
- Liquid purges or discharges from scrubbers used for atmospheric emission treatment. These purges usually contain high concentrations of salts and other compounds captured during gas washing.
Due to this wide variety of non-biodegradable contaminants, the most efficient solution is to identify and segregate those streams that may compromise the biological reactor’s operation and treat them using technologies specifically adapted to their composition.
Segregation of streams to protect the biological reactor and optimize treatment
Waters with a primarily biodegradable load can be directed to biological treatment, while concentrated, saline, toxic, inhibitory, or poorly biodegradable streams can be segregated for specific treatment.
This strategy allows:
- Protecting biomass from toxic or inhibitory substances.
- Avoiding excessive salt loads in the biological reactor.
- Reducing COD and contaminant load spikes.
- Maintaining more stable operating conditions.
- Improving the efficiency of biodegradable organic matter removal.
- Reducing the risk of performance loss or process destabilization.
- Applying the most suitable technology to each stream from a technical and economic standpoint.
Within this strategy, vacuum evaporation plays a particularly relevant role for the separate treatment of concentrated streams that are not convenient to incorporate directly into the biological process.
Treatment of biodegradable discharge
In general terms, biological treatments are the most widespread and economical alternative for industrial wastewater treatment.
For the biological treatment of these effluents, various technologies exist, including activated sludge systems, moving bed biofilm reactors (MBBR), anaerobic treatments, and specific processes for microcontaminant removal, among others.
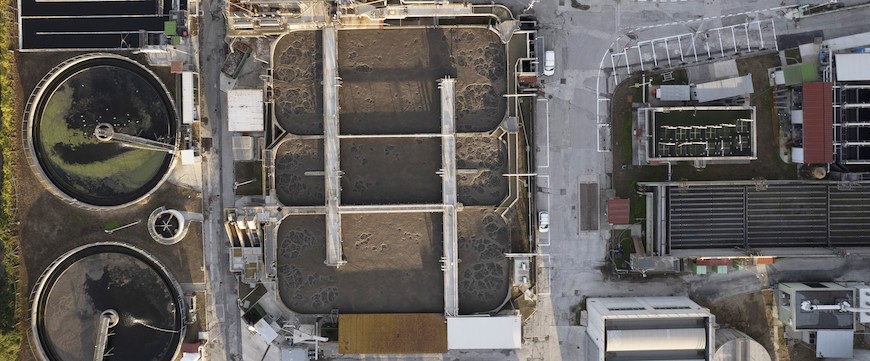
After proper segregation, the biological reactor should mainly receive streams with a sufficiently biodegradable organic fraction.
In a pharmaceutical plant, typically the following could be directed to the biological treatment:
- Wash and rinse waters from equipment, provided they are relatively dilute and do not contain problematic concentrations of API, disinfectants, or solvents.
- Waters from cleaning reactors, tanks, and pipelines after separating the first more concentrated fractions. Initial washes may carry much more product load, while subsequent rinses are usually more dilute.
- Effluents from processes with biodegradable organic matter, for example certain streams associated with fermentation or formulation processes, once their biodegradability has been verified.
- Waters with favorable BOD/COD ratios, where a sufficiently significant proportion of organic matter can be used by microorganisms.
- Streams previously treated by AOP or other pretreatment when toxicity has been reduced or refractory compounds transformed into more biodegradable substances.
- Effluents with traces of certain biodegradable APIs, provided resulting concentrations do not inhibit biomass and the biological process has demonstrated capacity to remove them.
As previously mentioned, in many cases these treatments face limitations due to the presence of inhibitory compounds.
Consequently, many pharmaceutical companies resort to authorized waste managers for the disposal of their liquid effluents, incurring high costs associated with transport and treatment.
In this context, vacuum evaporators have established themselves as one of the most efficient and cost-effective technologies for treating wastewater generated by the pharmaceutical industry, especially when dealing with effluents with high contaminant loads or difficult-to-treat compounds.
Vacuum evaporation for difficult-to-treat effluents
Vacuum evaporation is a thermal separation process that allows the removal of water and other solvents present in a liquid effluent by applying heat under reduced pressure conditions.
By lowering the pressure inside the evaporator, the boiling point of water is also reduced, allowing evaporation at temperatures considerably lower than atmospheric evaporation. This reduces energy consumption and minimizes thermal degradation of heat-sensitive compounds.
Thanks to these characteristics, vacuum evaporation has become one of the most used technologies for treating complex wastewater, especially in sectors such as pharmaceutical, chemical, or biotechnological industries.
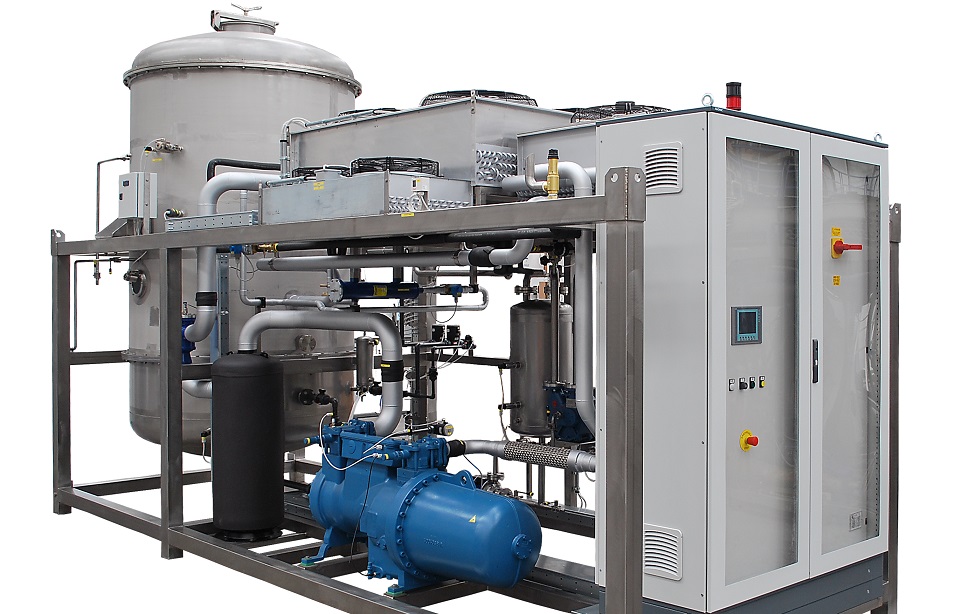
The role of vacuum evaporators in the pharmaceutical industry
In the pharmaceutical industry, this technology is especially interesting because it allows independent treatment of certain streams that, due to their composition, could be problematic for biological treatment.
Effluents with high salinity
Dissolved salts cannot be removed by conventional biological treatment and, when reaching high concentrations, can negatively affect biomass activity.
Evaporation allows separating a large part of the water from these streams while salts remain mostly concentrated in the reject.
This application can be especially interesting for certain scrubber purges and other saline streams generated during pharmaceutical processes, preventing their incorporation into the biological system from unnecessarily increasing the conductivity and salinity of the water received by the reactor.
Effluents with API and other low biodegradability compounds
Pharmaceutical active ingredients and other microcontaminants may have low biodegradability and, in certain cases, exert inhibitory effects on microorganisms.
Evaporation allows removing these streams from the biological circuit and concentrating most contaminants in a considerably smaller volume.
Although evaporation does not necessarily imply destruction of APIs, their concentration in a reduced stream facilitates subsequent management or treatment by other technologies, such as advanced oxidation, adsorption, or crystallization.
When compound and process characteristics allow, the obtained concentration can also facilitate recovery of active ingredients or other valuable products.
Effluents with solvents
Solvents are another type of stream that requires differentiated management, as certain solvent concentrations can cause a high COD load and inhibit biomass activity.
In complex aqueous streams where solvents appear along with salts, APIs, and other contaminants and the main goal is to reduce waste volume, vacuum evaporation can be an appropriate alternative. In these cases, a properly designed thermal separation strategy can allow separation or recovery of certain solvents, reducing both the contaminant load to be managed later and raw material consumption.
When solvent concentration and value justify it, the preferred alternative may be the use of solvent distillers that allow selective separation and recovery of one or more solvents with sufficient purity for reuse.
In the pharmaceutical industry, it is possible to recover solvents with very high purities, with processes specifically designed to recover THF, methanol, ethyl acetate, or DMSO from residual streams.
The following table shows in which scenarios one or the other alternative is preferable:
| Stream type | Technology usually most suitable |
|---|---|
| Stream rich in a recoverable solvent | Distillation / vacuum distillation for solvent recovery |
| Mixture of several solvents and water | Multistage distillation, extractive or other specific separation, depending on azeotropes and VLE equilibrium |
| Wastewater with small amounts of solvents + salts + API + other contaminants | Vacuum evaporator, possibly with vapor/distillate treatment |
| Saline or refractory COD stream where the goal is volume reduction | Vacuum evaporation |
| Process stream where raw material recovery is also of interest | It is advisable to study solvent recovery before treating the remaining residue |
Design must be specifically carried out for the considered mixture, taking into account aspects such as volatility, boiling point, azeotrope formation, process safety, and real recovery possibilities.
Concentrated effluents with high non-biodegradable COD
High COD does not necessarily imply that an effluent can be biologically treated.
When a significant part of that COD corresponds to refractory substances, introducing the stream into the biological reactor increases the contaminant load without necessarily providing a substrate that microorganisms can degrade.
Segregating these streams avoids unnecessarily overloading biological treatment and allows treating them by evaporation or other technologies specifically designed for refractory contaminants.
Vacuum evaporation as a protective barrier for the biological reactor
The function of a vacuum evaporator in a pharmaceutical plant goes beyond treating complex effluents and reducing waste volume.
A treatment stage using a vacuum evaporator allows isolating the biological reactor from streams with high salinity, toxicity, low biodegradability, or high concentrations of certain contaminants.
A conceptual treatment configuration can be:
Pharmaceutical process → stream segregation → specific treatment of problematic effluents → biological treatment of biodegradable streams → final treatment/reuse
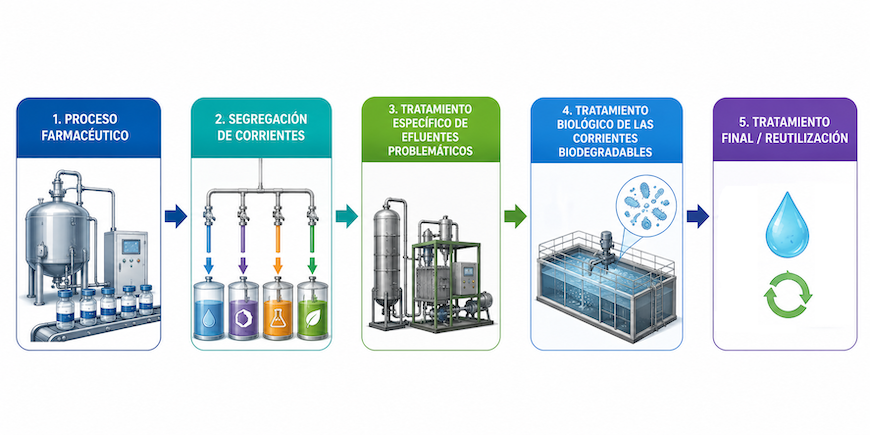
With this solution, biological treatment is used precisely where it is most efficient: in the removal of biodegradable organic matter. Meanwhile, effluents that could compromise its operation receive specific treatment.
This combination allows designing more robust plants, reducing load fluctuations received by biomass, and optimizing the overall treatment cost.
Main benefits of installing a vacuum evaporator in a pharmaceutical WWTP
Concentration of contaminants and minimization of waste volume
During evaporation, water turns into vapor while most organic and inorganic contaminants remain in the concentrate.
As a result, the volume of liquid waste that must later be managed or treated by other technologies is significantly reduced, decreasing both transport costs and costs associated with disposal.
Additionally, this concentration facilitates the separation of a significant part of the contaminants present in the effluent.
Recovery of valuable products
In certain applications, concentrated compounds retain high economic value and can be recovered for reuse within the production process.
This is the case for numerous active pharmaceutical ingredients (API), solvents, or raw materials used during drug manufacturing.
Recovery of these products requires a carefully controlled evaporation process, with specific temperature, pressure, and residence time conditions to avoid degradation or loss of properties of the recovered compounds.
Concentration of microcontaminants
Although vacuum evaporation does not completely destroy microcontaminants, it does allow concentrating them in a smaller volume stream.
This concentration facilitates their subsequent removal by complementary technologies such as adsorption, advanced oxidation, crystallization, or certain specialized filtration processes.
Recovery and reuse of water
The distillate generated by evaporation can have high quality. Depending on the initial effluent composition, contaminant volatility, and subsequent treatment applied, this water can be reused in certain auxiliary services within the plant.
Thus, evaporation can simultaneously contribute to reducing liquid waste volume and fresh water consumption.
Protection of biological treatment
Segregation and evaporation of highly saline, inhibitory, refractory, or concentrated streams prevent these contaminants from reaching the biological reactor.
This promotes greater biomass stability and reduces the risk of performance loss caused by peak loads or substances incompatible with the biological process.
Limitations of vacuum evaporation
Although vacuum evaporation is a very effective technology for treating pharmaceutical effluents, it also presents certain limitations that must be considered during treatment plant design.
- Complexity of effluents: Wastewaters from the pharmaceutical industry may contain a very diverse combination of active pharmaceutical ingredients (API), chemicals, salts, solvents, surfactants, and microcontaminants. This complexity means that, in certain applications, evaporation alone is not sufficient to achieve the required treatment goals.
- Concentrate management: One of the main objectives of evaporation is to concentrate contaminants present in the reject, minimizing the volume of waste that must be sent to an authorized manager. However, this concentrate still contains a high contaminant load and must be properly managed to avoid any environmental impact.
- Microcontaminant removal: Evaporation allows concentrating microcontaminants but does not always completely remove them. When the goal is their destruction or mineralization, it is usually necessary to incorporate complementary technologies capable of degrading these compounds.
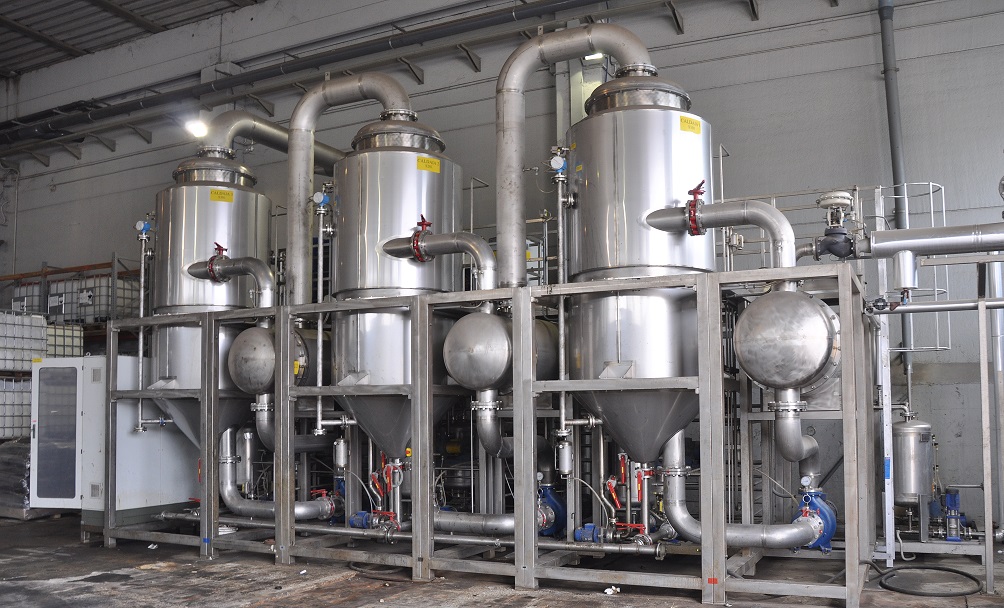
Advanced oxidation processes (AOP)
Advanced Oxidation Processes (AOP) are very efficient in treating wastewater containing persistent organic compounds, microcontaminants, or substances that are difficult to biodegrade by conventional processes.
Their operation is based on generating highly reactive species, mainly hydroxyl radicals, capable of oxidizing a wide variety of organic contaminants and transforming complex molecules into simpler compounds. Among the most used technologies are:
- Fenton processes and their variants
- Ozonation
- Different combinations of oxidants, ultraviolet radiation, and catalysts.
In the pharmaceutical industry, AOPs are especially interesting due to the potential presence of active pharmaceutical ingredients (API), antibiotics, and other refractory organic compounds that may have low biodegradability and be difficult to remove by conventional treatments.
AOPs are usually integrated with other technologies within a treatment train due to their high energy and reagent consumption. Depending on effluent characteristics and treatment goals, two configurations are especially interesting for pharmaceutical wastewater:
- The combination of advanced oxidation with biological treatment
- Combination of advanced oxidation with vacuum evaporation.
Advanced oxidation processes (AOP) + biological treatment
Advanced Oxidation Processes (AOP) have demonstrated high effectiveness in treating wastewater from the pharmaceutical industry, especially when containing emerging contaminants, refractory compounds, or substances difficult to biodegrade.
These technologies use oxidizing agents capable of generating hydroxyl radicals (•OH), extremely reactive species that degrade complex organic compounds into simpler, biodegradable molecules.
Thanks to this process, AOPs reduce Chemical Oxygen Demand (COD) and break down the molecular structure of numerous organic contaminants, facilitating their subsequent removal by conventional biological treatments.
This strategy is especially interesting economically, as it does not aim to completely mineralize all organic matter using chemical reagents, but to increase its biodegradability so that subsequent biological treatment completes the process with lower reagent consumption and reduced operating cost.
Advanced Oxidation Processes are based on physicochemical mechanisms capable of causing profound modifications in the chemical structure of contaminants through hydroxyl radical generation (•OH), considered one of the most powerful oxidizing agents available for wastewater treatment.
The formation of these radicals can be obtained from different combinations of oxidants, such as oxygen, hydrogen peroxide (H2O2), ozone, ultraviolet radiation, or specific catalysts, depending on the technology used. As a result, the main final oxidation products are usually water, carbon dioxide, and other compounds with lower environmental impact.
Among the most used technologies are Fenton processes and their different variants. These processes consist of adding iron salts that act as catalysts in the presence of hydrogen peroxide (H2O2) and under controlled pH, temperature, and reaction time conditions, promoting the formation of hydroxyl radicals capable of oxidizing a wide variety of organic contaminants.
Once the advanced oxidation stage is completed, the effluent can undergo conventional biological treatment. In many cases, this combination allows meeting discharge limits established by regulations and even obtaining water quality sufficient for reuse in certain auxiliary services within the pharmaceutical plant itself.
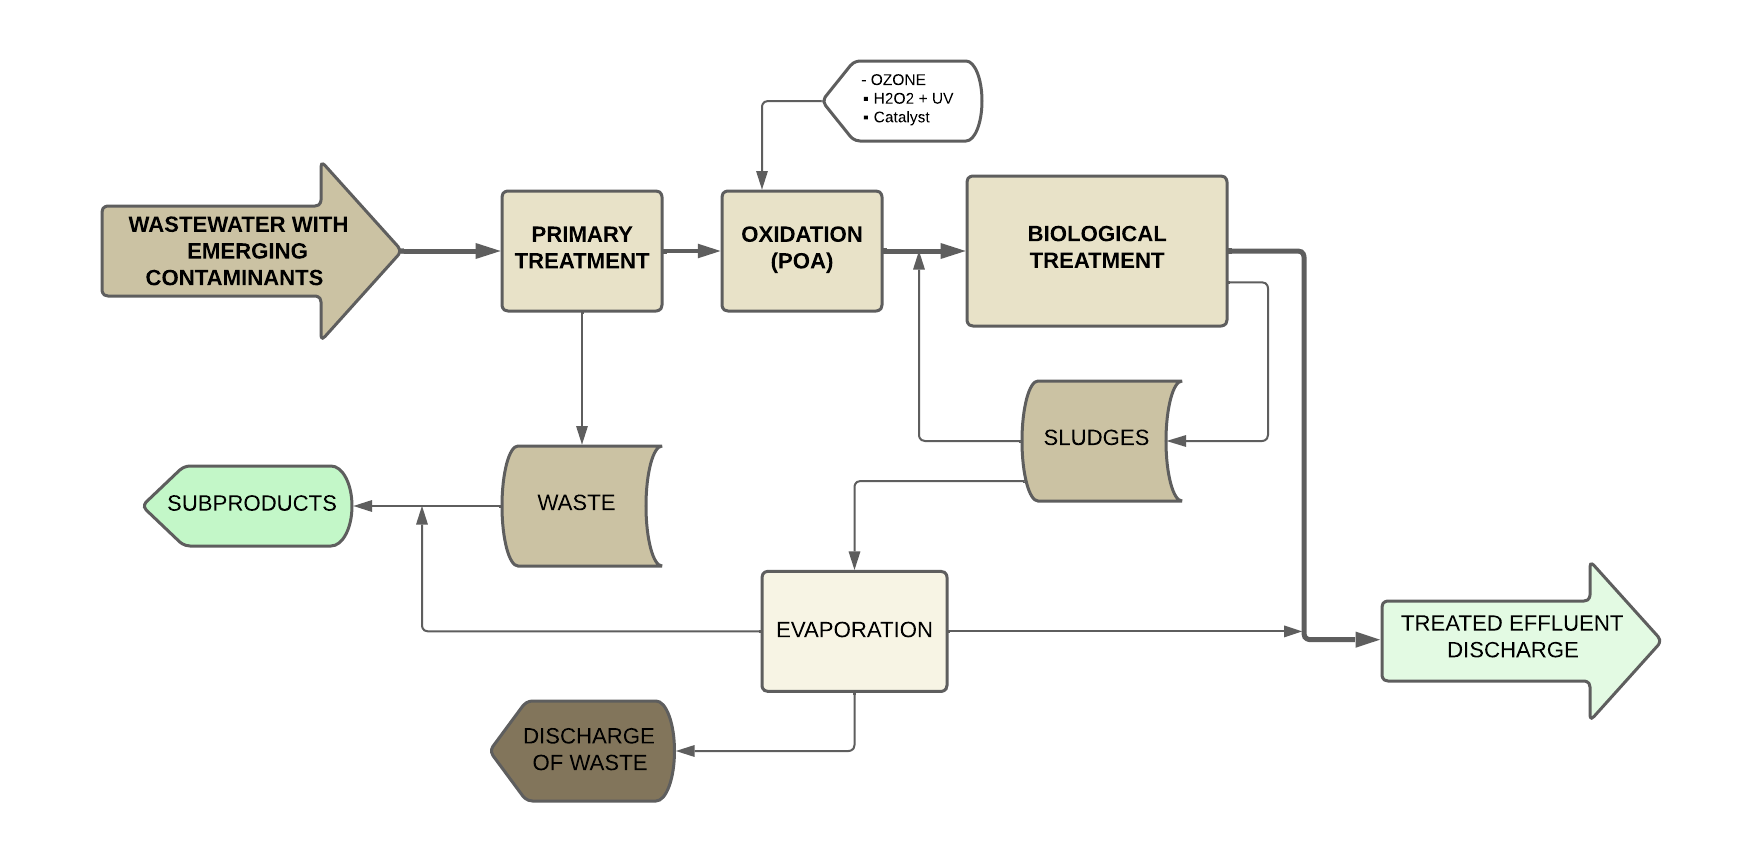
Advanced oxidation (AOP) + vacuum evaporation
The combination of Advanced Oxidation Processes (AOP) and vacuum evaporation is one of the most effective solutions for treating wastewater generated by the pharmaceutical industry, especially when effluents have high concentrations of organic contaminants, refractory compounds, or microcontaminants difficult to remove by conventional technologies.
Advanced Oxidation Processes use hydroxyl radicals (•OH), highly reactive species capable of oxidizing a wide variety of organic compounds. Their main advantages include a high capacity to degrade persistent contaminants and, in many cases, partially or totally mineralize them into carbon dioxide, water, and other compounds with lower environmental impact.
However, advanced oxidation also has certain limitations, mainly related to reagent consumption and energy requirements, especially when treating effluents with high organic matter concentrations.
For this reason, it is common to combine AOPs with other technologies that optimize overall process performance and reduce operating costs.
Vacuum evaporation effectively complements advanced oxidation by concentrating contaminants present in the effluent through water evaporation. Besides significantly reducing liquid waste volume, this process facilitates recovery of certain valuable compounds and decreases the load that subsequent stages must treat.
Integrating both technologies allows leveraging the advantages of each. While AOPs degrade the most complex organic compounds and increase effluent biodegradability, evaporation concentrates remaining contaminants and minimizes the volume of generated reject.
As a result, a highly efficient treatment system is obtained, especially suitable for small flows with high contaminant loads, a very common situation in many pharmaceutical manufacturing processes.
The need for a personalized and integrated solution for each case
In practice, vacuum evaporation is usually part of a comprehensive treatment strategy. The high diversity of streams generated in the pharmaceutical industry makes it difficult to establish a single technology valid for all effluents.
The solution involves analyzing which contaminants each stream contains, their concentrations, and which technology is most suitable to remove, separate, or recover them.
Biological treatments remain an efficient solution for biodegradable streams.
Advanced Oxidation Processes can be used to degrade certain refractory contaminants or increase their biodegradability.
Vacuum evaporation allows separating and concentrating complex, saline, or poorly biodegradable streams, as well as offering possibilities for recovering water, solvents, APIs, or other valuable products.
Depending on effluent characteristics, these processes can be combined with other industrial wastewater treatment technologies such as physicochemical processes, adsorption, crystallization, or membrane processes to achieve purification, reuse, or discharge objectives.
The key is to properly segregate different effluents at their source and prevent the most problematic streams from compromising the operation of the rest of the treatment plant.
This approach enables developing more robust, efficient treatment systems adapted to the real characteristics of each pharmaceutical process.

