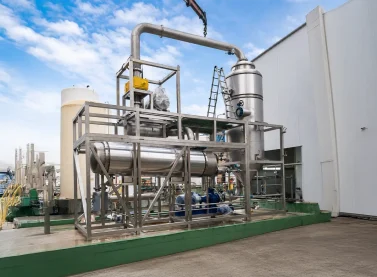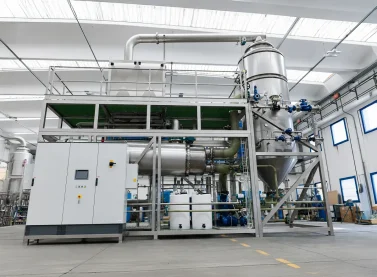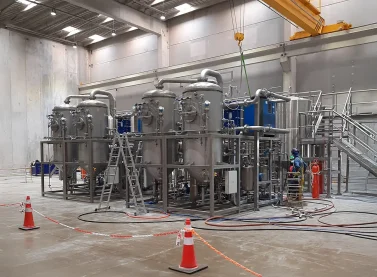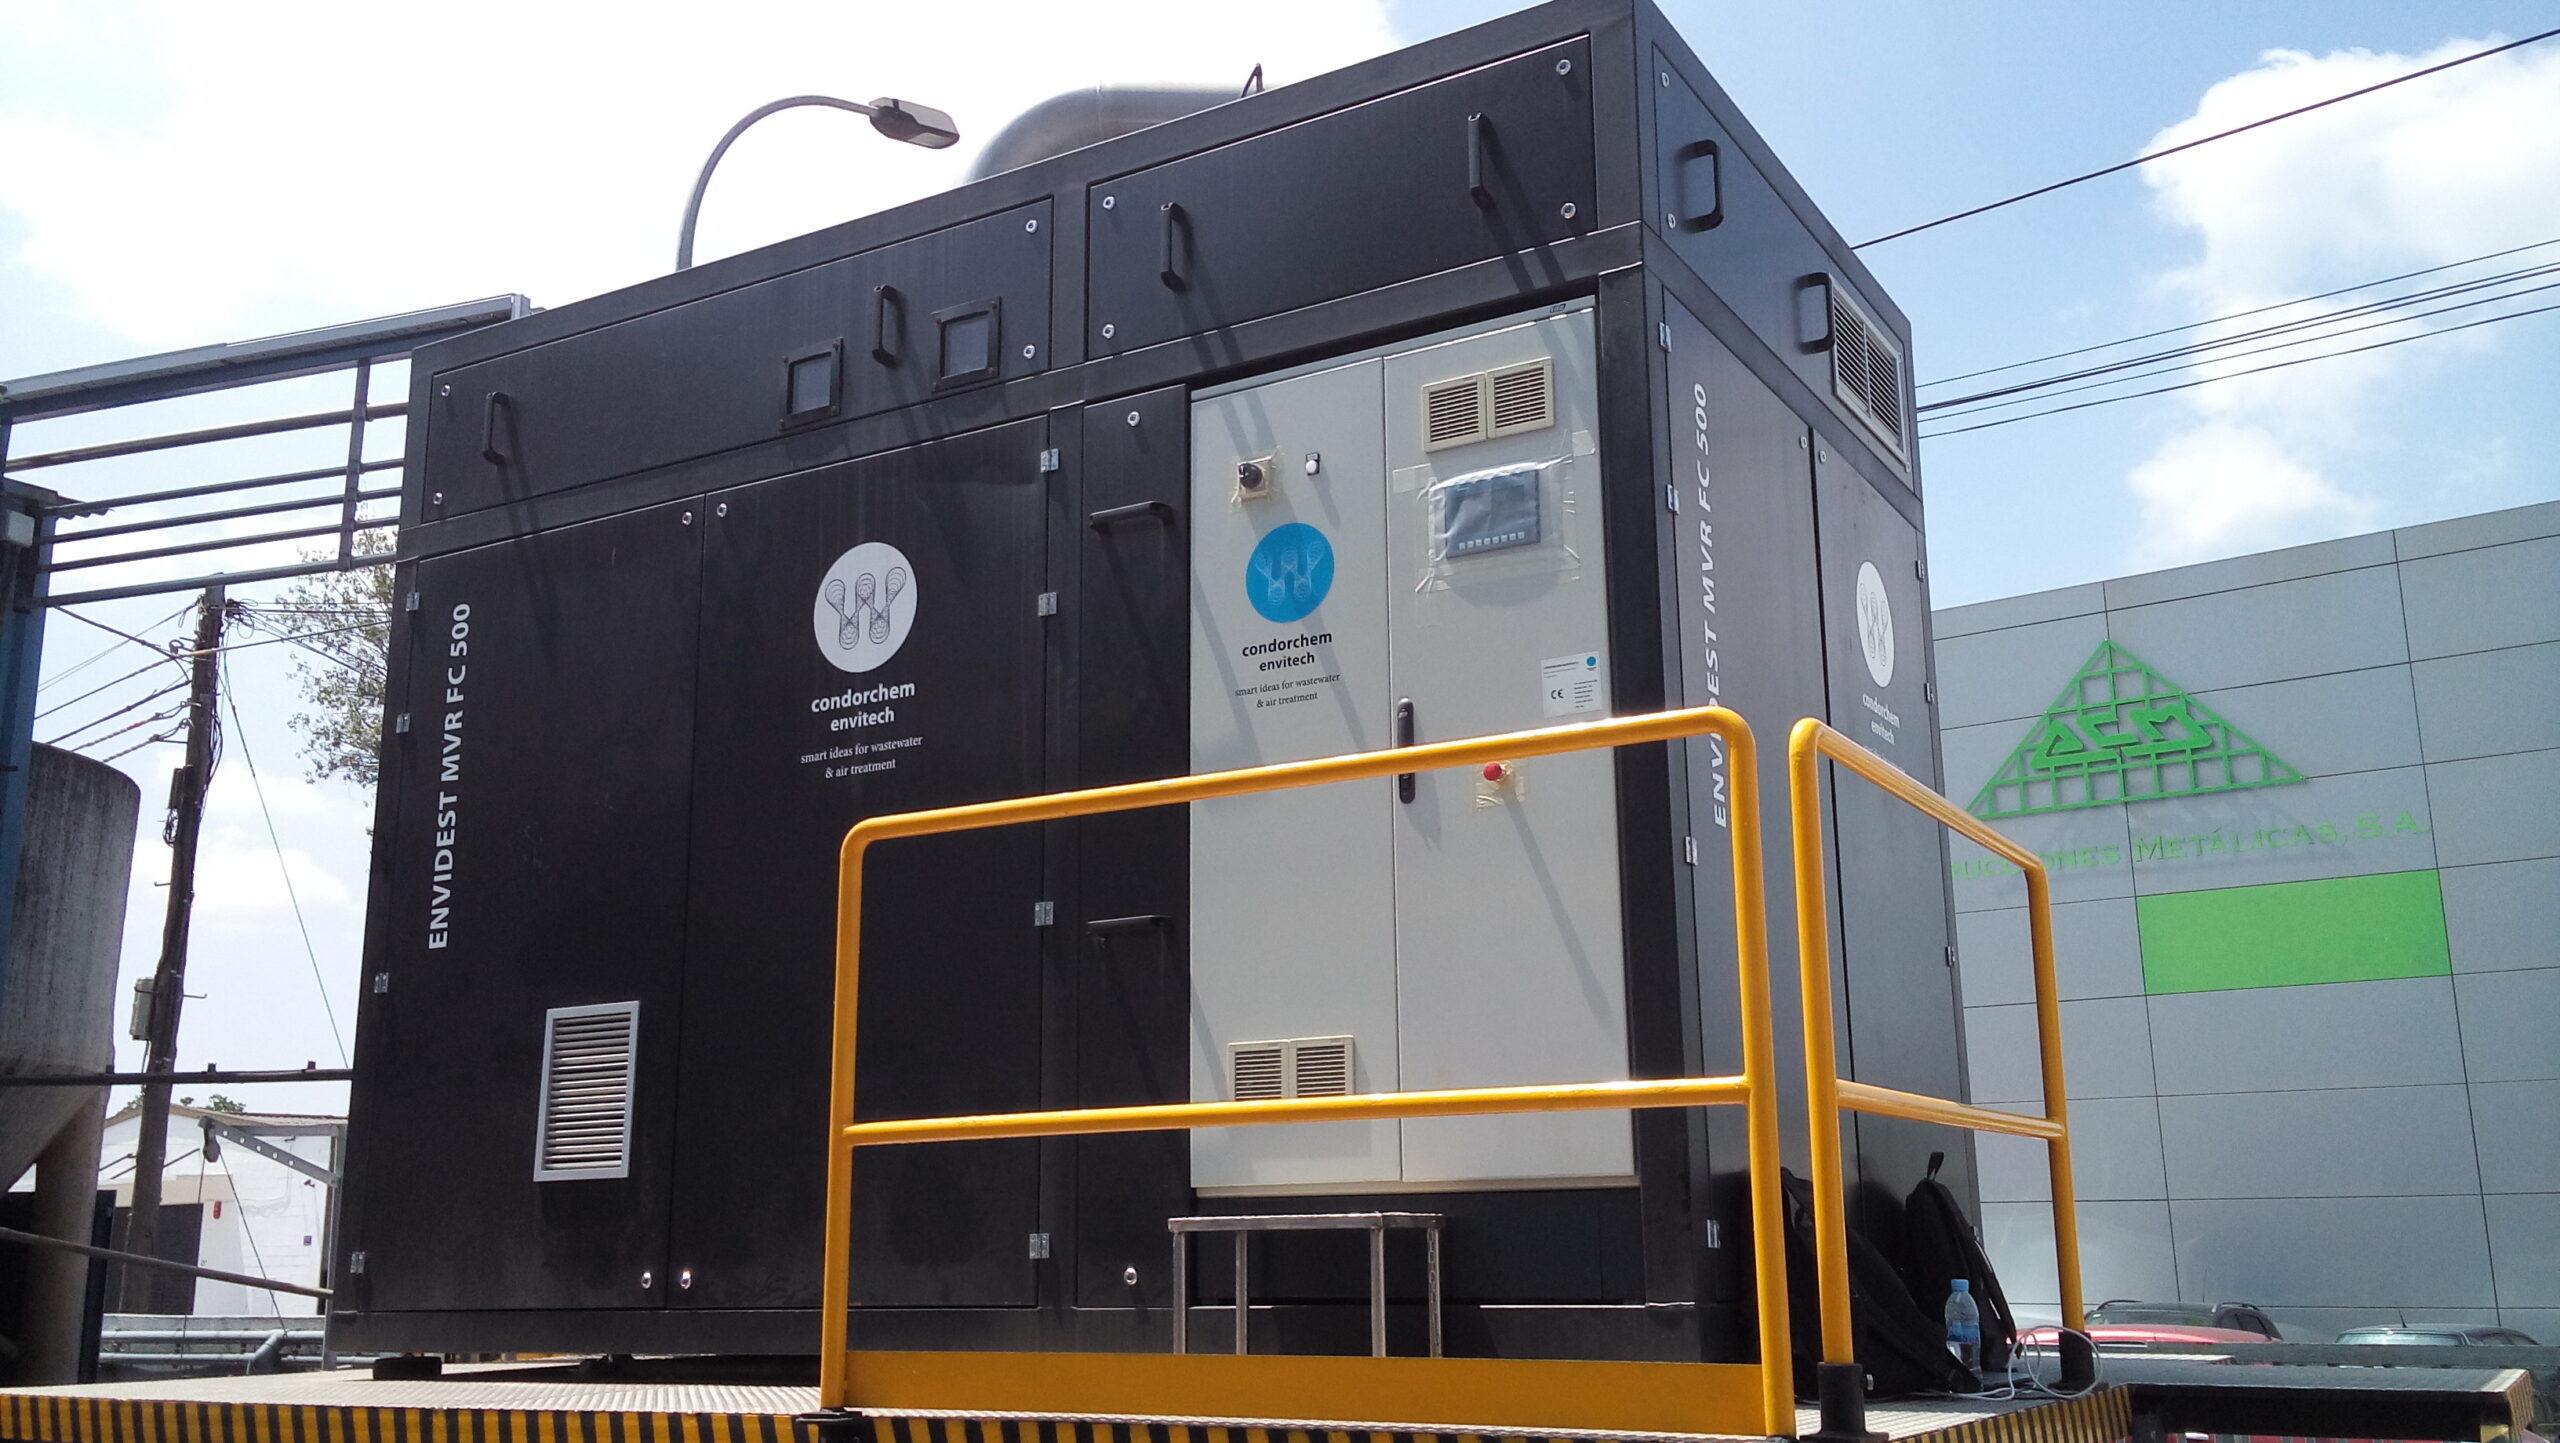
- The widest capacity range
- They can operate with thermal or electrical energy
- One, two, and three effects available
MODELS AND MAIN TECHNICAL FEATURES
We design and manufacture different models of forced-circulation vacuum evaporators, enabling us to adapt to different flow rates, pollutant loads, and energy sources.
Our range spans from compact heat pump units to multiple-effect evaporation systems for treating large volumes of industrial wastewater. Additionally, we manufacture mechanical vapor recompression (MVR) evaporation systems, which are ideal for reducing energy consumption and optimizing operating costs.
Forced-circulation evaporators keep the effluent continuously moving through the heat exchanger, reducing the formation of deposits and enabling the treatment of high-viscosity effluents. This technology is especially recommended for treating highly viscous liquid waste with a high tendency to fouling and scaling, containing crystals, suspended solids, or salts that hinder natural circulation.
At Condorchem Enviro Solutions, we offer a wide range of vacuum evaporators for treating all types of industrial effluents.
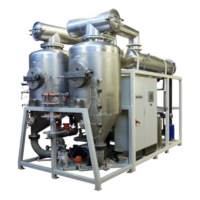
Technology: Heat Pump (Freon R-513A) / Forced Circulation (FC)
Capacity (l/day): 6720 to 52800
Electricity consumption per 1 m³ of distillate produced: 110 kWh/m³
Vacuum: ≈ 120/70 mbar
Evaporation temperature: ≈ 50/40 °C
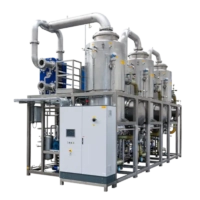
Technology: Forced Circulation (FC) thermal energy evaporation
Capacity (l/day): 20000 to 200000
Electricity consumption per 1 m³ of distillate produced: 20 to 110 kWh/m³
Thermal energy for evaporation: 630 to 2100 kWht
Thermal energy for condensation: 630 to 2100 kWht
Vacuum (1st/2nd/3rd Effect): ≈ 310/200/125 mbar
Evaporation temperature (1st/2nd/3rd Effect): ≈ 70/60/50°C
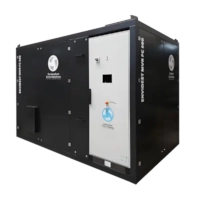
Technology: Mechanical Vapor Recompression (MVR) / Forced Circulation (FC)
Capacity (l/h): 1042 to 4166
Electricity consumption per 1 m³ of distillate produced: 35 kWh/m³
Vacuum: ≈ 750 mbar
Evaporation temperature: ≈ 90-94 °C
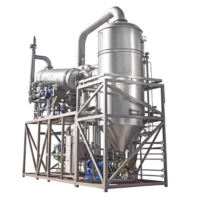
Technology: Thermal energy evaporation / Forced Circulation (FC)
Capacity (l/day): 20000 to 100000
Electricity consumption per 1 m³ of distillate produced: 26 to 48 kWh/m³
Thermal energy for evaporation: 630 to 3140 kWht
Thermal energy for condensation: 630 to 3140 kWht
Vacuum (1st/2nd/3rd Effect): ≈ 200 mbar
Evaporation temperature (1st/2nd/3rd Effect): ≈ 60°C
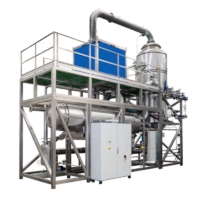
Technology: Mechanical Vapor Recompression (MVR) / Forced Circulation (FC)
Capacity (l/h): 600 to 2500
Power consumption per 1 m³ of distillate produced: 64 kWh/m³
Vacuum: ≈ 700 mbar
Evaporation temperature: ≈ 90 °C
FORCED CIRCULATION EVAPORATOR AND CRYSTALLIZER SELECTION
Compare the available configurations according to the effluent characteristics, required capacity, available energy and the concentration or crystallization objective.
| Application or priority | Recommended model | Selection criterion | Nominal capacity* | Energy and electricity consumption |
|---|---|---|---|---|
| Low-temperature concentration of effluents with a low pollutant load. | ENVIDEST LT FC-2 | Double-effect heat pump with evaporation temperatures of approximately 50 and 40 °C. Forced circulation handles somewhat more scaling effluents than units with a submerged exchanger. | 6,720–52,800 L/day | 110 kWh/m³ of distillate |
| Treatment of oily water or streams with a low pollutant load where space is limited. | ENVIDEST MVR FF | Combines falling film and forced circulation in a compact unit, with components that are accessible for maintenance. | 120–1,980 L/h | 35–60 kWh/m³ of distillate |
| Concentration of larger flows of effluents with a low pollutant load using MVR. | ENVIDEST MVR FC TF | Combines a turbocompressor with high-velocity recirculation to limit deposits in the shell-and-tube exchanger. | 1,042–4,166 L/h | 35 kWh/m³ of distillate |
| Concentration of large flows when low-cost heat is available. | ENVIDEST MFE 1 | A single evaporation stage. Suitable when the thermal savings of a second effect do not justify the additional investment. | 20,000–130,000 L/day | Steam or hot water. Single effect. |
| Concentration of large effluent volumes with lower external heat demand. | ENVIDEST MFE 2 | The vapor from the first effect heats the second. A pump at each stage keeps the liquid circulating. | 30,000–120,000 L/day | Steam or hot water. Double effect. |
| Treatment of large volumes when operating hours and heat cost justify a third effect. | ENVIDEST MFE 3 | Reuses heat over three stages and offers the highest nominal capacity in the range. | 30,000–200,000 L/day | Steam or hot water. Triple effect. |
| Concentration of effluents with a high pollutant load and salt crystallization using MVR. | DESALT MVR FC | Designed to precipitate dissolved salts. Recirculation limits scaling in the exchanger. Requires an auxiliary supply of saturated steam. | 600–2,500 L/h | 64 kWh/m³ of distillate |
| Salt crystallization for large volumes of effluents with a high pollutant load when a suitable heat source is available. | DESALT MFE-1 | High-velocity recirculation helps control scaling. The inclined exchanger makes it easier to drain during shutdowns. | 20,000–100,000 L/day | Steam or hot water. Single effect, with cooling water for condensation. |
* Nominal evaporation capacities with clean water under standard conditions. Each data sheet’s units are kept: L/h or L/day. The actual effluent flow treated depends on its composition and the required final concentration.
In addition to flow rate, viscosity, scaling tendency, the presence or formation of crystals and the available energy should be assessed. ENVIDEST models are aimed at evaporation and concentration; the DESALT models in this table are designed to enable salt crystallization.
MAIN OPERATIONAL ADVANTAGES
- Forced-circulation evaporators are the most efficient for treating viscous liquids, as they maintain intense circulation inside the equipment, even with concentrated effluents.
- They reduce scale formation, as the high speed at which the liquid moves reduces deposits on the heat-transfer surfaces.
- They allow operation with suspensions and streams prone to crystallization.
- High concentration levels are achieved, reducing the volume of waste for external management or final crystallization.
MAIN COMPONENTS OF EACH MODEL
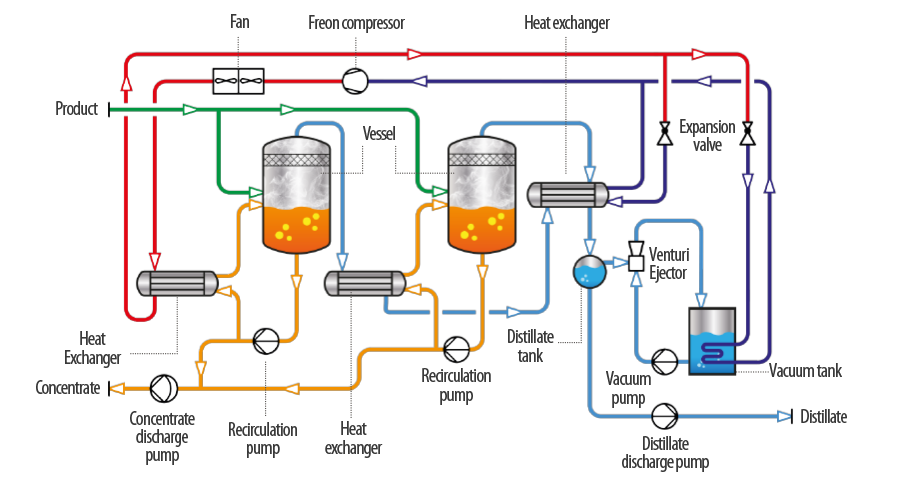
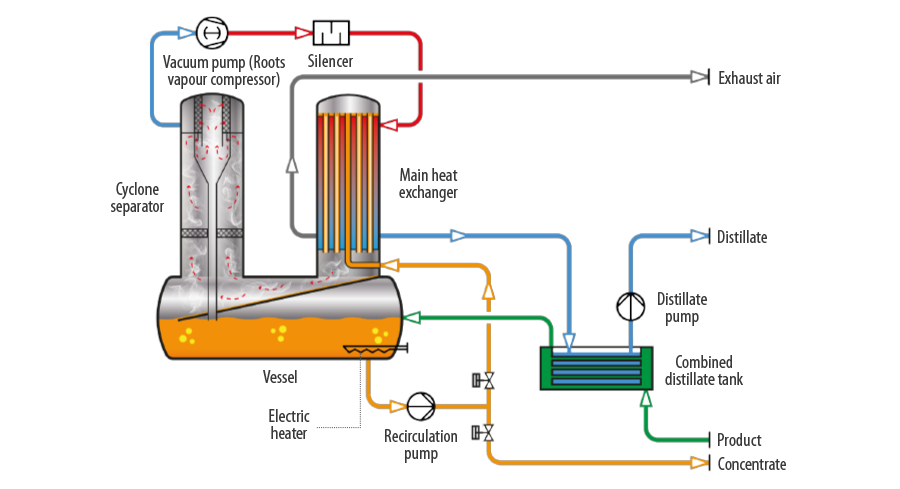
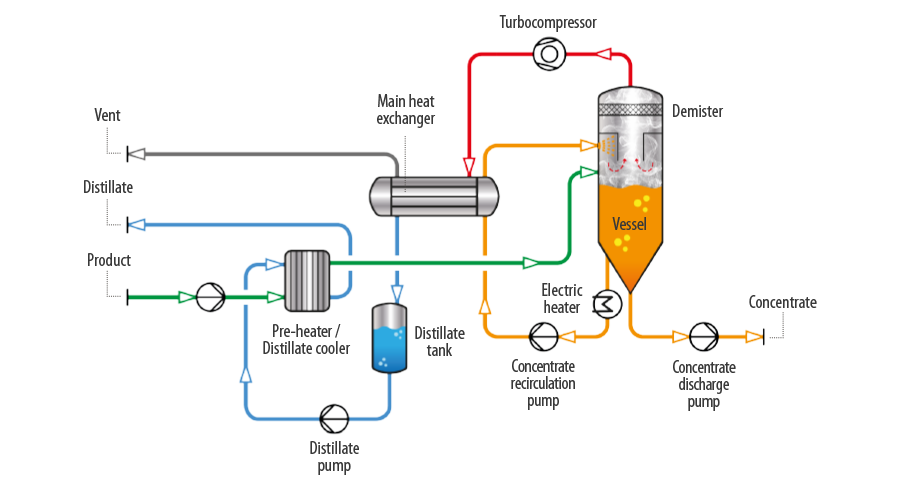
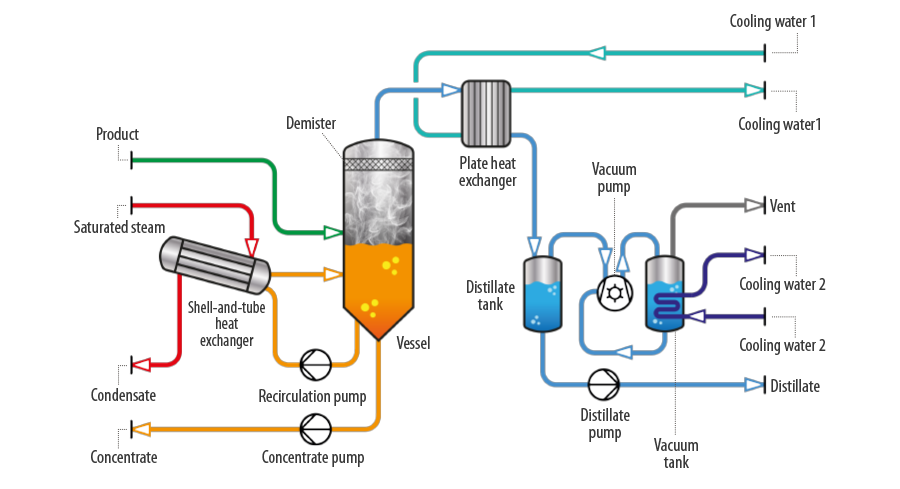
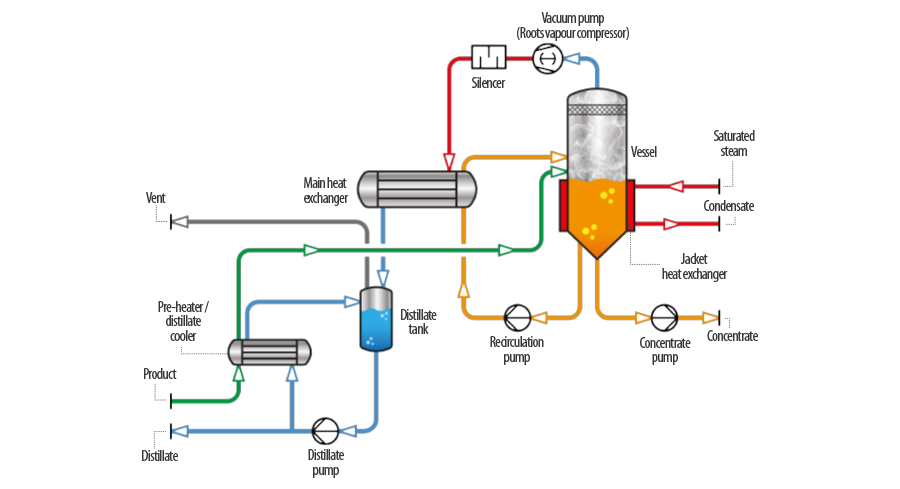
The following video shows the DESALT MVR FC evaporator/crystallizer. The video details all the equipment components and the main operational advantages of crystallization systems using mechanical vapor recompression.
OPERATION OF OUR FORCED-CIRCULATION VACUUM EVAPORATORS
Start-up and filling
When the evaporator is switched on, the feed valve opens and the effluent or product to be treated begins to fill the vessel chamber.
Forced circulation
Once the level is reached, the recirculation pump is activated to create a constant flow of liquid through the heat exchanger and its corresponding vessel, ensuring effective heat transfer and the handling of complex streams that would otherwise quickly foul or choke the process.
Circuit Heating
For thermal evaporators, whether using saturated steam or hot water, jackets are used to reach the operating temperature.
Electric evaporators use a series of electrical heating elements inside the vessel to achieve the same result.
Circulation and condensation
Once the entire circuit has reached operating temperature, the boiler vapors pass through the heat exchangers and condense to recover the distillate. During the process, heat is recovered and used to heat the new product introduced into the equipment for treatment.
3D VIDEO ANIMATION
The following video shows a 3D animation detailing, step by step, how our forced-circulation MVR evaporators work.
CONFIGURATIONS
Our forced-circulation evaporators can be manufactured in different CONFIGURATIONS:
- Energy source: electric or thermal
- Single-, double-, or triple-effect evaporators.
In this way, each evaporator can be adapted to the flow rate to be treated, the availability of energy, the operating cost, and the investment budget of each project.
Thermal evaporators are the most suitable option for large treatment capacities, especially when a residual heat source is available.
Single-effect systems are the most cost-effective alternative for low flow rates or when the aim is to minimize the initial investment. In contrast, double- and triple-effect configurations reuse the latent heat generated during evaporation, significantly reducing the process’s energy consumption and operating cost.
Electric evaporators, for their part, stand out for their flexibility, ease of installation, and high efficiency when treating a wide range of flow rates, especially when space is limited.